You ensure oats are safe down to parts per million by combining tight supply-chain controls with validated analytical methods, then releasing lots only when sampling, extraction, and measurement consistently demonstrate gluten below the relevant limit (often <20 ppm, sometimes stricter).
This article walks through what “ppm” really means for oats, why oats are harder to test than most foods, which methods hold up under oat-specific performance requirements, and how a serious QA program closes the gap between a clean Certificate of Analysis and real-world consumer trust. You’ll also see where certifications fit, where they do not, and how to build a testing plan that survives audits, investigations, and hot-spot risk.
How Do You Test Oats For Gluten Down To “Parts Per Million” (Ppm)?
When a gluten-free oat claim has to stand up in the U.S. market, the testing workflow starts with a simple truth: the result is only as credible as the sample. Gluten contamination in oats tends to appear as “rare events” (a stray wheat, barley, or rye kernel) rather than a uniform smear. That reality turns ppm testing into a two-part problem, grabbing a sample that represents the lot, then measuring gluten accurately in that sample.
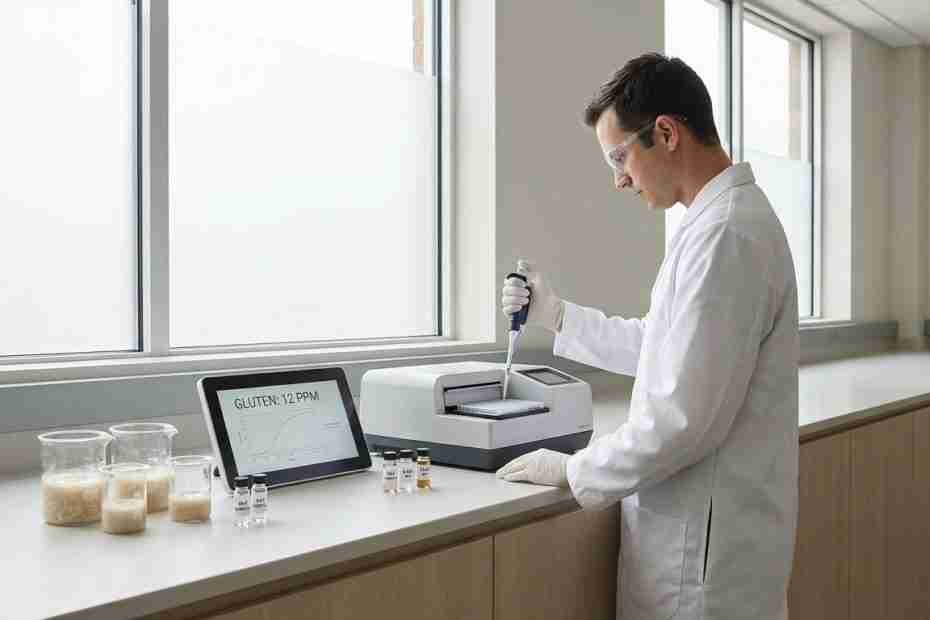
Operationally, ppm is just mg/kg, so a lab instrument is not “detecting a label claim,” it is quantifying a mass fraction. The industry workhorse is immunoassay testing (ELISA), which uses antibodies to bind gluten proteins or fragments and converts that binding signal into a concentration. For oat programs, you typically treat ELISA as the high-throughput decision tool for lot release, with confirmatory or investigative tools used when results look inconsistent or when disputes arise.
To reach low ppm performance with any credibility, the lab has to control pre-analytics with discipline: milling to a consistent particle size, homogenizing thoroughly, preventing cross-contact in the prep area, and standardizing extraction chemistry and time. Oats push extraction harder than many matrices, and incomplete extraction is a silent failure mode that can produce reassuring numbers that do not reflect the true contamination. Serious programs validate the extraction and matrix behavior at the facility level, not just on a kit insert.
On the analytics side, you will commonly see sandwich ELISA formats used for intact gluten proteins, paired with matrix-appropriate extraction steps. Labs that do investigative work may use LC-MS/MS approaches to detect gluten peptides and, in some cases, support grain-source identification in mixed events. LC-MS/MS tends to be positioned as an advanced tool for confirmation, root-cause work, or method dispute resolution, not the routine tool for every production lot due to cost, throughput, and expertise constraints.
What Does 20 Ppm Gluten-Free Mean, And Is 20 Ppm “Safe” For Oats?
In the United States, “gluten-free” on a food label has a regulatory meaning: the food must contain less than 20 parts per million of gluten, and the formulation cannot intentionally use ingredients that are gluten-containing grains (wheat, rye, barley, or their crossbreeds) or non-removed derivatives. That 20 ppm figure is not a marketing convention, it is the compliance line that FDA uses for enforcement and misbranding decisions. It also reflects what FDA described as the lowest level that could be consistently detected with valid analytical tools when the rule was established.
What 20 ppm means in practice depends on serving size and consumption pattern. A 30 g serving of oats at 20 ppm represents a different gluten mass exposure than a 90 g “big bowl” used daily, even though the ppm number is the same. This is why experienced QA leaders avoid talking as if “20 ppm” automatically equals “no risk,” and instead talk about measured compliance, process control, and exposure management for high-consumption foods.
For oats, the question is rarely just “Is the mean below 20 ppm,” it is “Is the lot reliably below 20 ppm when contamination is inhomogeneous?” This is where a well-built sampling plan and a decision rule matter. If a company runs one quick test on one grab sample and calls it a day, the program is not aligned with oat reality. If a company designs a multi-increment sampling plan, mills and homogenizes properly, runs replicates, and uses hold-and-release logic, the 20 ppm requirement becomes a real operational control point rather than a hopeful statement.
Many brands choose stricter internal targets than 20 ppm for oats, not because FDA requires it, but because oats create trust pressure in the market. The tighter the internal action limit, the more testing and process capability are required to keep false fails manageable and maintain supply continuity. That trade-off is a business choice, but it has to be made with a clear view of what the test method can reliably do at the low end and how much lot variability is expected.
What’s The Difference Between “Gluten-Free Oats” And “Purity Protocol Oats”?
“Gluten-free oats” is a claim about the finished product meeting the regulatory threshold, while “purity protocol” is a supply-chain design that aims to prevent gluten grains from entering the oat stream in the first place. In purity protocol programs, controls typically begin at seed selection and continue through field management, harvest, transport, storage, and processing. The intention is prevention, supported by verification testing, rather than reliance on post-hoc sorting plus testing.
In contrast, many conventional systems rely on mechanical and optical sorting to remove foreign grains from a mixed stream, followed by testing to show that the cleaned output meets a limit. Sorting can be effective, yet it is not magic; it is still a process with escape risk, especially when contaminants share similar size or optical signatures. Oats raise the stakes because one escaped kernel can create a hot spot that is not captured if sampling is too shallow or grinding is inconsistent.
From a QA standpoint, the cleanest way to compare these systems is by asking where control authority lives. Purity protocol shifts control upstream and reduces dependence on end-product testing to “catch everything,” while sorting-driven programs rely heavily on final verification and the probability that sampling will detect rare events. A strong program can exist in either model, but the sampling intensity, lot definition, and decision rules typically have to be stricter in sorting-driven systems to compensate for the higher probability of localized contamination.
Many manufacturers blend the two philosophies. They implement upstream supplier requirements that look a lot like purity protocol controls, then still run aggressive receiving and finished-goods testing because oats are an audit magnet and a consumer-trust hotspot. That layered control is where mature programs land, prevention where possible, verification everywhere it matters.
Which Gluten Test Methods Are Considered Validated For Oats, And What Ppm Can They Reliably Detect?
For oat matrices, generic “gluten ELISA” language is not enough. Oat-specific method expectations exist because oats behave differently in sampling and because different grains and protein fractions can behave differently in antibody-based methods. AOAC’s Standard Method Performance Requirements for quantitation of wheat, rye, and barley gluten in oats specify performance expectations including a limit of detection and limit of quantitation at or below 5 ppm, and an analytical range beginning at or below 5 ppm. This matters because it forces method developers and labs to demonstrate low-end performance in oat flour rather than claiming sensitivity in an easier matrix.
Those requirements also acknowledge a painful truth: method results for gluten in oats can be highly variable due to sample inhomogeneity, and antibody specificity differences across wheat, rye, and barley complicate balanced response. That is why the SMPR recovery criteria are wider than what many analysts expect at low ppm levels. From an industry operator viewpoint, this is not an academic detail, it is a warning label for your QA system: do not build a release program that assumes oat samples behave like a uniform powder.
On the method side, collaborative studies are the credibility currency that separates “works in one lab” from “works across the industry.” The AOAC collaborative study for an ELISA method (First Action 2018.15) demonstrated performance in oat and oat product matrices and reported a measurement range beginning at 5 mg/kg (ppm) with multi-lab participation. That kind of data supports the argument that the method can operate in the low ppm space when used correctly, and it gives auditors a documented basis for method suitability.
LC-MS/MS approaches can complement immunoassays by targeting specific peptide markers and supporting more detailed investigative work. The operational caution is that LC-MS/MS is still only as good as extraction and sample representation, and it introduces its own complexity in method development, standards, and interpretation. The best programs use LC-MS/MS intentionally, as a confirmatory or investigative layer, not as a replacement for well-run routine lot testing.
Why Do People Say “Gluten-Free Oats Still Make Me Sick” Even If They Test Under 20 Ppm?
When consumers report problems with gluten-free oats, QA teams tend to jump to testing failure or supplier failure. That is sometimes correct, yet oats create multiple plausible explanations that a responsible program has to treat separately. One category is true gluten exposure from cross-contact that was not captured by sampling, or that occurred after testing due to handling, rework, or packaging-line cross-contact. Another category is that the lot is compliant on average but contains rare high-gluten particles that a given consumer happens to ingest, which is a hot-spot problem, not a mean-value problem.
Oats also trigger sensitivity discussions that are not strictly the same as wheat/rye/barley gluten exposure. Within the celiac community, some individuals report not tolerating oats even when they are labeled gluten-free and certified. From a manufacturing standpoint, it is critical not to overpromise what gluten testing can guarantee. Gluten testing verifies wheat/rye/barley gluten contamination against a limit; it does not guarantee every consumer will tolerate every oat product, and it cannot guarantee the absence of rare-event spikes unless the sampling plan is designed to manage that risk aggressively.
This is where communicating “how the testing is done” matters. If a brand can describe lot definition, sampling intensity, milling and homogenization controls, and decision rules, the story becomes credible. If the message is only “we test,” it reads like a checkbox and does not address what experienced consumers worry about. When consumer trust is under pressure, the program has to show competence in the unglamorous steps, sampling, prep, and lot discipline.
Internally, this issue should trigger a QA review that treats complaints as signals, not nuisances. That review should examine trending by supplier, by plant line, by packaging format, and by production schedule adjacency to gluten-containing products. If the program finds no correlation and the lots were managed with strong controls, the brand can communicate with confidence about what was measured and how release decisions were made.
Do Third-Party Certifications Test To Lower Than 20 Ppm (Like 10 Ppm Or 5 Ppm)?
Third-party certification can add discipline, yet it is not a substitute for owning the QA system. In the U.S., the FDA limit for a gluten-free claim is <20 ppm, but some certification programs advertise stricter thresholds, along with audits and oversight requirements. When a program sets a lower action level, it forces stronger process control, tighter supplier management, and more careful interpretation of low-end analytical variability.
The practical value of certification is not only the number printed in program marketing. It is the operational requirements that come with it: supplier qualification, traceability expectations, audit cadence, corrective action follow-up, and how the program handles disputes or market investigations. These features matter because the biggest failures in oat programs rarely come from a single test kit choice; they come from weak lot definition, poor segregation, inadequate sampling, and inconsistent execution under schedule pressure.
Certifications also shape how consumers interpret risk. Many consumers look for recognizable certification marks because they want an external control signal, not just a brand promise. That creates a responsibility: if certification is used as a trust anchor, the manufacturer’s internal program must be at least as strong as the certification requirements, and it must remain strong during supply disruptions when procurement pressure rises.
When designing a program, treat certification thresholds as one input into your action limits, not the only input. If oat intake is high or the product is targeted to a sensitive consumer base, the business case for tighter internal limits becomes clearer. The trade-off is that tighter limits require more sampling and more repeat testing to avoid false rejects and to manage unavoidable low-end analytical noise.
What’s Going On With The “Gluten-Free Oats Controversy”, And Are Any Brands Actually Safe Right Now?
The oat category has faced repeated cycles of consumer concern, third-party testing claims, and brand or certifier responses. The core technical driver is not mystery, it is the combination of cross-contact risk in grain systems and the hot-spot behavior of contaminants that can evade shallow sampling. When an advocate group reports elevated findings, the follow-on debate often centers on lot identity, sampling method, lab accreditation, method selection, extraction, and whether the tested samples represented the released lots.
From an operator’s seat, the right question is not “Who is right on social media,” it is “What program design survives independent scrutiny?” That means you need documented supplier controls, defensible sampling plans, validated methods aligned to oat matrices, and a release process that is not vulnerable to one-off convenience decisions. It also means retaining retains, keeping chain-of-custody records, and being ready to re-test with an accredited third-party lab if claims emerge.
Brands can be safe when their systems are engineered for oat reality, and when procurement, operations, and QA share authority to stop shipment on uncertainty. At the same time, no program should claim perfection. The honest, durable stance is that safety is managed by prevention, verification, and rapid corrective action, with transparent explanation of what was measured and how the lot was controlled. Consumers can then decide with clear information rather than vague reassurance.
If a company wants to lead in this category, it has to treat oats as a high-risk ingredient relative to many other naturally gluten-free grains. That means more supplier audits, more receiving scrutiny, stricter segregation, and more frequent verification testing. When that investment is real, the category becomes manageable. When it is not, controversy becomes predictable.
How You Build A Release-Ready Gluten Testing Program That Holds Up In Audits
A defensible gluten-free oat program starts with a written objective tied to regulatory and customer requirements. In the U.S., you need the capability to demonstrate that lots labeled gluten-free are below 20 ppm gluten and that your formulation does not intentionally include prohibited gluten-containing grains. Then you translate that requirement into control points: supplier qualification, incoming ingredient verification, in-process controls, finished-goods verification, and traceable lot release criteria.
Lot definition is a quiet failure point. If the “lot” is too large, you dilute risk and create false confidence because your sample represents only a tiny fraction of the total. If the lot is too small, you raise testing cost and slow throughput. The right lot definition is built around process reality: defined supplier lots, defined silo or bin boundaries, defined production windows, and defined packaging runs with clear segregation from any gluten-containing operations.
Sampling is where programs win or lose credibility. A single grab sample is weak for oats; strong programs use multi-increment sampling from across the lot, then combine and homogenize to create a composite that reflects the lot more reliably. This is also where milling matters. You are not testing whole oats in a bag with an ELISA directly; you are typically testing a milled, homogenized lab sample, and the homogeneity of that lab sample drives repeatability.
Decision rules should be written before results arrive. If the internal limit is 10 ppm, the program needs a documented rule for what happens at 8 ppm, 10 ppm, 12 ppm, or a result near the LOQ. Replicate testing rules, hold-and-investigate triggers, and third-party confirmation triggers should be pre-defined so results are not negotiated in real time. Auditors and sophisticated customers look for that discipline because it signals that the program is engineered, not improvised.
How Sampling And Homogenization Decide Whether “Ppm” Means Anything At All
In oat testing, sampling error often exceeds instrument error. That statement frustrates people who want a single definitive number, yet it is the operational reality. If contamination enters as kernels, fragments, or localized dust, the distribution is not uniform. A lab can run a perfect ELISA on a non-representative sample and still produce a result that misrepresents the lot.
To reduce that risk, you need a sampling plan with breadth. That means collecting increments from multiple locations across bags, totes, or bulk handling points, not just from the top layer or one convenient access point. In bulk systems, it means sampling during flow, at defined intervals, rather than relying on static probes in settled material. The goal is not to “get a sample,” it is to approximate the probability distribution of contaminants within the lot.
Homogenization is the second gate. If milling produces a non-uniform flour with clumps or particle-size separation, the sub-sample weighed into extraction can vary dramatically. Strong labs control mill type, mill cleanliness, sieve conditions if used, and blending time, and they document that control. In audits, those records often matter as much as the test result because they show the lab understands oat behavior.
If you need a practical internal check, run replicate analyses from the same milled composite. When replicate variability is large, the program should not treat the average as comfort. It should treat variability as a signal that the sample or homogenization is unstable or that hot spots are present. That is when additional increments, re-milling, or tighter lot segmentation becomes the right move.
How ELISA Actually Works In Oats, And Where It Can Mislead You
ELISA methods measure gluten based on antibody binding. The signal is converted to concentration by calibration, and results are typically reported as mg/kg, which equals ppm. The strength of ELISA is throughput, relative cost, and practicality for routine lot release. The weakness is that antibodies see what they are designed to see, and extraction chemistry determines what becomes visible to those antibodies.
Oats complicate ELISA in a few ways. Contaminants may be wheat, rye, or barley, each with protein fractions that can behave differently in extraction and antibody recognition. Methods and requirements that explicitly target wheat/rye/barley gluten in oats exist because performance can vary by grain source and because oat matrices can increase variability. AOAC’s oat-focused SMPR calls out this variability and the role of antibody specificity differences as reasons performance criteria differ from typical expectations at ppm levels.
Another operational trap is treating a single ELISA kit selection as the whole program. Kit choice matters, yet kit selection does not fix shallow sampling, poor milling, rushed extraction, or cross-contact in the lab. When investigations happen, the root cause is frequently one of those execution problems. A well-run ELISA program looks boring on paper: controlled sample prep, controlled extraction, controlled calibration, controls on every run, and clear acceptance criteria.
When a result is near the limit, ELISA should trigger process discipline, not argument. Replicates, re-sampling, confirmation at an accredited third-party lab, and review of the sample chain-of-custody should be standard. If a brand needs to ship product, the pressure will arrive. Your job is to have pre-written rules that prevent pressure from becoming a quality decision.
How LC-MS/MS Fits When You Need Confirmation Or Grain-Specific Answers
LC-MS/MS is often discussed as the “more advanced” option, yet it should be treated as a targeted tool, not a blanket replacement for ELISA. The practical reason is throughput and cost, but the deeper reason is that LC-MS/MS does not eliminate sampling risk. If the sample misses the contaminant kernel, the instrument sophistication does not rescue the result.
Where LC-MS/MS earns its place is in confirmation and investigation. When you have conflicting results, a complaint cluster, or a public claim that a product exceeded limits, LC-MS/MS can provide an independent analytical angle. It can detect specific peptide markers and can support a stronger technical explanation of what is present in a sample when the story is contested. Published work describes gluten detection and speciation using LC-MS/MS approaches, supporting the idea that mass spectrometry can complement immunoassays when questions get hard.
In a mature QA program, LC-MS/MS is written into escalation paths. The trigger conditions are defined, the lab partner is pre-qualified, and the chain-of-custody is locked down. This prevents the common failure where a company scrambles for a method only after an issue goes public. If oats are part of your core portfolio, pre-planning this layer is a strategic advantage.
When using LC-MS/MS, insist on method clarity. Ask what markers are used, what calibration strategy is used, what the stated LOD/LOQ is in your matrix, and what extraction protocol is used. Treat it as a scientific measurement, not a magic stamp.
How Certifications, Audits, And Lab Accreditation Support (Or Undermine) Trust
Trust is built when controls are repeatable and independently verifiable. Lab accreditation and audits matter because they reduce the chance that a program is built on informal habits. Accreditation signals that a lab has documented competence, validated methods, and quality systems around instruments, analysts, and reporting. Audits signal that a plant has a living food safety and allergen control system, not just paperwork.
That said, certification marks do not guarantee perfect execution at every moment. A certified program can still experience supply disruptions, staffing changes, equipment issues, or segregation failures. This is why your internal program must be designed to detect drift. Verification sampling, trend reviews, periodic third-party checks, and supplier re-qualification keep the system honest between formal audit points.
When public disputes occur, the difference between brands that recover quickly and brands that spiral is documentation discipline. Retain samples, chain-of-custody logs, lot genealogy, and test records allow fast, credible re-testing and investigation. If those records are incomplete, the brand is forced into vague statements that reduce trust. Oats are a category where record quality is part of the product.
Use audits as training opportunities for operational teams. When operators understand why the sampling plan is designed the way it is, shortcuts become less likely. When operators see “ppm testing” as a lab-only activity, the plant becomes the weak link. A successful oat program is a plant culture, not a lab activity.
Ppm Release Decisions: How You Set Action Limits, Retest Rules, And Hold Criteria
Once testing is in place, release decisions become the core of the program. If the label claim is “gluten-free,” the U.S. compliance line is <20 ppm, yet many companies set internal action limits below that for oats. The right internal limit depends on consumption level, brand promise, certification commitments, and the statistical behavior of your supply chain. Lower internal limits demand better sampling and often more testing, or the program will get stuck in retest loops and false rejects.
Retesting is where many programs quietly fail. If retesting is used to “get a passing number,” the program will eventually ship a problem lot. Retesting should be used to reduce uncertainty, not to negotiate outcomes. Your SOP should state when retesting is allowed, how many replicates are run, how new samples are collected, how results are interpreted near the LOQ, and when third-party confirmation is required.
Hold criteria should be decisive. If a lot shows high variability between replicates, treat that as risk, not noise. If a lot is near the limit and the product is a high-consumption oat item, the program should default to hold and investigate. This is where executive support matters; the QA leader needs authority to hold product without fear of retaliation for schedule disruption.
Documented decision rules also protect customer service and brand communication. When consumers ask “How do you know,” you can answer with process facts: lot definition, sampling plan, method used, controls used, and release criteria. That answer is more durable than reassurance and helps reduce misinformation when controversies flare.
How Do You Ensure Gluten-Free Oats Are Below 20 Ppm?
- Prevent cross-contact upstream, then verify with multi-point sampling
- Mill and homogenize, then test with oat-validated methods
- Hold and re-test lots near limits, release only when results are consistent
Make Your Oat Testing Claims Audit-Proof
You earn credibility in gluten-free oats by treating sampling as a scientific control, using oat-appropriate validated methods, and enforcing release rules that do not bend under operational pressure. FDA’s <20 ppm definition sets the compliance baseline, yet oats demand more discipline because contamination can be uneven and method performance varies at low levels. AOAC’s oat-focused performance requirements and collaborative method work underscore that this category needs careful execution, not casual “we test” messaging. When you combine upstream prevention, disciplined lab prep, and clear hold-and-release criteria, you turn ppm into a meaningful safety control rather than a fragile number. If oats are a priority product line, build the program so it stays stable during supply disruptions, investigations, and the next wave of consumer scrutiny.